
Custom Molded Seals
When no catalogue seal fits — custom injection or compression molded seals from concept to production.
Overview
Highly specialized seals for every industry
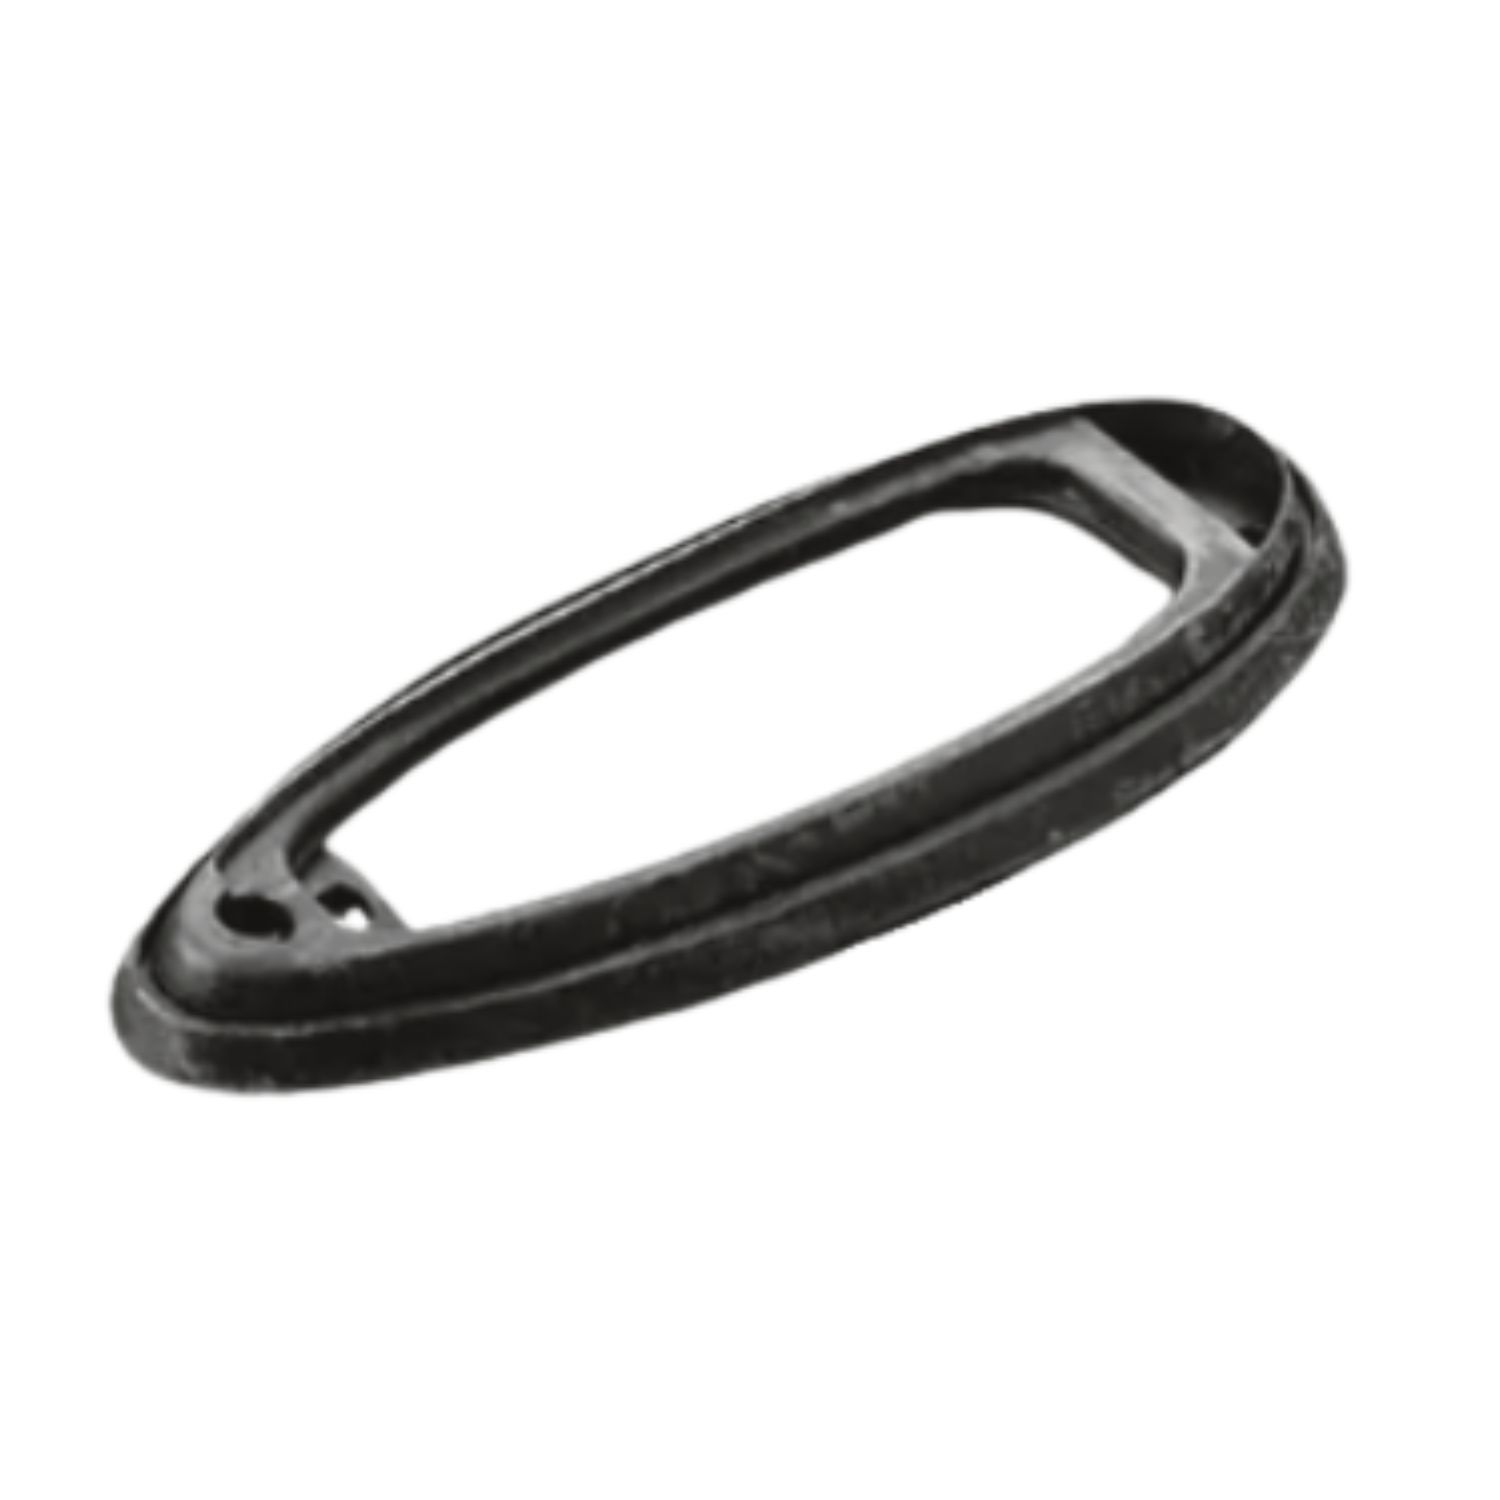
Custom molded seals are specified when the sealing function requires a geometry that cannot be achieved with standard profiles — complex cross-sections, integrated multiple lips, over-molded metal inserts, bellows geometries, or seals that must perform multiple simultaneous functions in a single molded component.
We collaborate on seal design from project conception through to production approval. If you have an application where every off-the-shelf seal has failed, or you're designing new equipment and need a sealing element that doesn't exist yet, that's the kind of problem custom molding solves.
Materials include nitrile (NBR), EPDM, silicone (VMQ), fluoroelastomers (FKM), urethane, and solid thermoplastics. Two primary manufacturing methods are used depending on part geometry, material, and production volume: injection molding and compression molding.
Manufacturing
Injection molding & compression molding
The injection molding process
Injection molding heats the elastomer or thermoplastic compound to a flowable state, then injects it under high pressure into a multi-cavity mold. The mold geometry defines the part geometry with repeatable precision — every part from the first to the ten-thousandth is dimensionally identical.

| Process Step | Description |
|---|---|
| 1. Compound preparation | Raw elastomer compound mixed to exact formulation. Shore hardness, chemical resistance, and temperature range set at this stage. |
| 2. Injection | Compound heated to liquid state and injected under pressure into the mold cavities. Pressure and temperature profile precisely controlled. |
| 3. Cure / vulcanization | Heat initiates crosslinking in the elastomer matrix. This is the step that gives rubber its elastic recovery and mechanical strength. |
| 4. Demolding | Part ejected from mold after full cure cycle. Multi-cavity molds produce multiple identical parts per cycle. |
| 5. Deflashing | Removal of flash at parting lines. Critical for sealing applications — flash in a sealing groove prevents compression. |
| 6. Inspection | Dimensional check, visual inspection, and functional testing per approved inspection plan. |
Compression molding — the alternative for complex elastomers
Compression molding places a pre-measured charge of uncured compound directly into an open mold cavity. The mold closes under hydraulic pressure, forcing the material to fill the cavity as heat initiates vulcanization. While slower per cycle than injection molding, compression molding handles compounds with very high viscosity, produces very low residual stress in the finished part, and is the preferred method for large cross-section seals, diaphragms, and parts with undercuts that cannot be injection-molded.

| Criterion | Injection Molding | Compression Molding |
|---|---|---|
| Material viscosity | Low to medium — compound must flow under injection pressure | High viscosity compounds — material does not need to flow, just compress and fill |
| Part complexity | High — multi-cavity, tight tolerances, complex geometry | Moderate — large cross-sections, diaphragms, seals with thick sections |
| Cycle time | Shorter — faster for high-volume production | Longer — preferred for specialty compounds and large-volume parts |
| Flash | Minimal — parting line flash only | More flash typical — deflashing step required |
| Tooling cost | Higher — precision injection tooling | Lower — simpler mold construction for moderate volumes |
| Best for | High-volume precision seals, O-rings, lip seals, multi-lip profiles | Diaphragms, large gaskets, specialty elastomers (FFKM, silicone sponge), prototype quantities |
Design flexibility — shape, size, and complexity
Injection molding accommodates geometry that is impossible in extruded or cut gaskets: complex 3D shapes, varying cross-sections, grooves and undercuts, bellows features, and integrated functional elements.

| Design Feature | Capability |
|---|---|
| Cross-section complexity | Multiple thicknesses, grooves, bevels, lips, channels, and bellows in a single part. No limitation from standard profile libraries. |
| Size range | Miniature (sub-millimeter cross-section) to oversized components (>500 mm diameter). Mold size and injection press capacity are the only constraints. |
| Tolerances | Tight tolerances achievable with precision molds. Better repeatability than extruded or cut seals for critical dimensions. |
| Metal inserts | Metal components can be over-molded — integrate metal reinforcement, bonded metal faces, or threaded inserts directly into the molded rubber part. |
| Multi-material | Co-injection and two-shot molding available for parts requiring different materials in different zones — e.g., rigid thermoplastic body with soft sealing lip. |
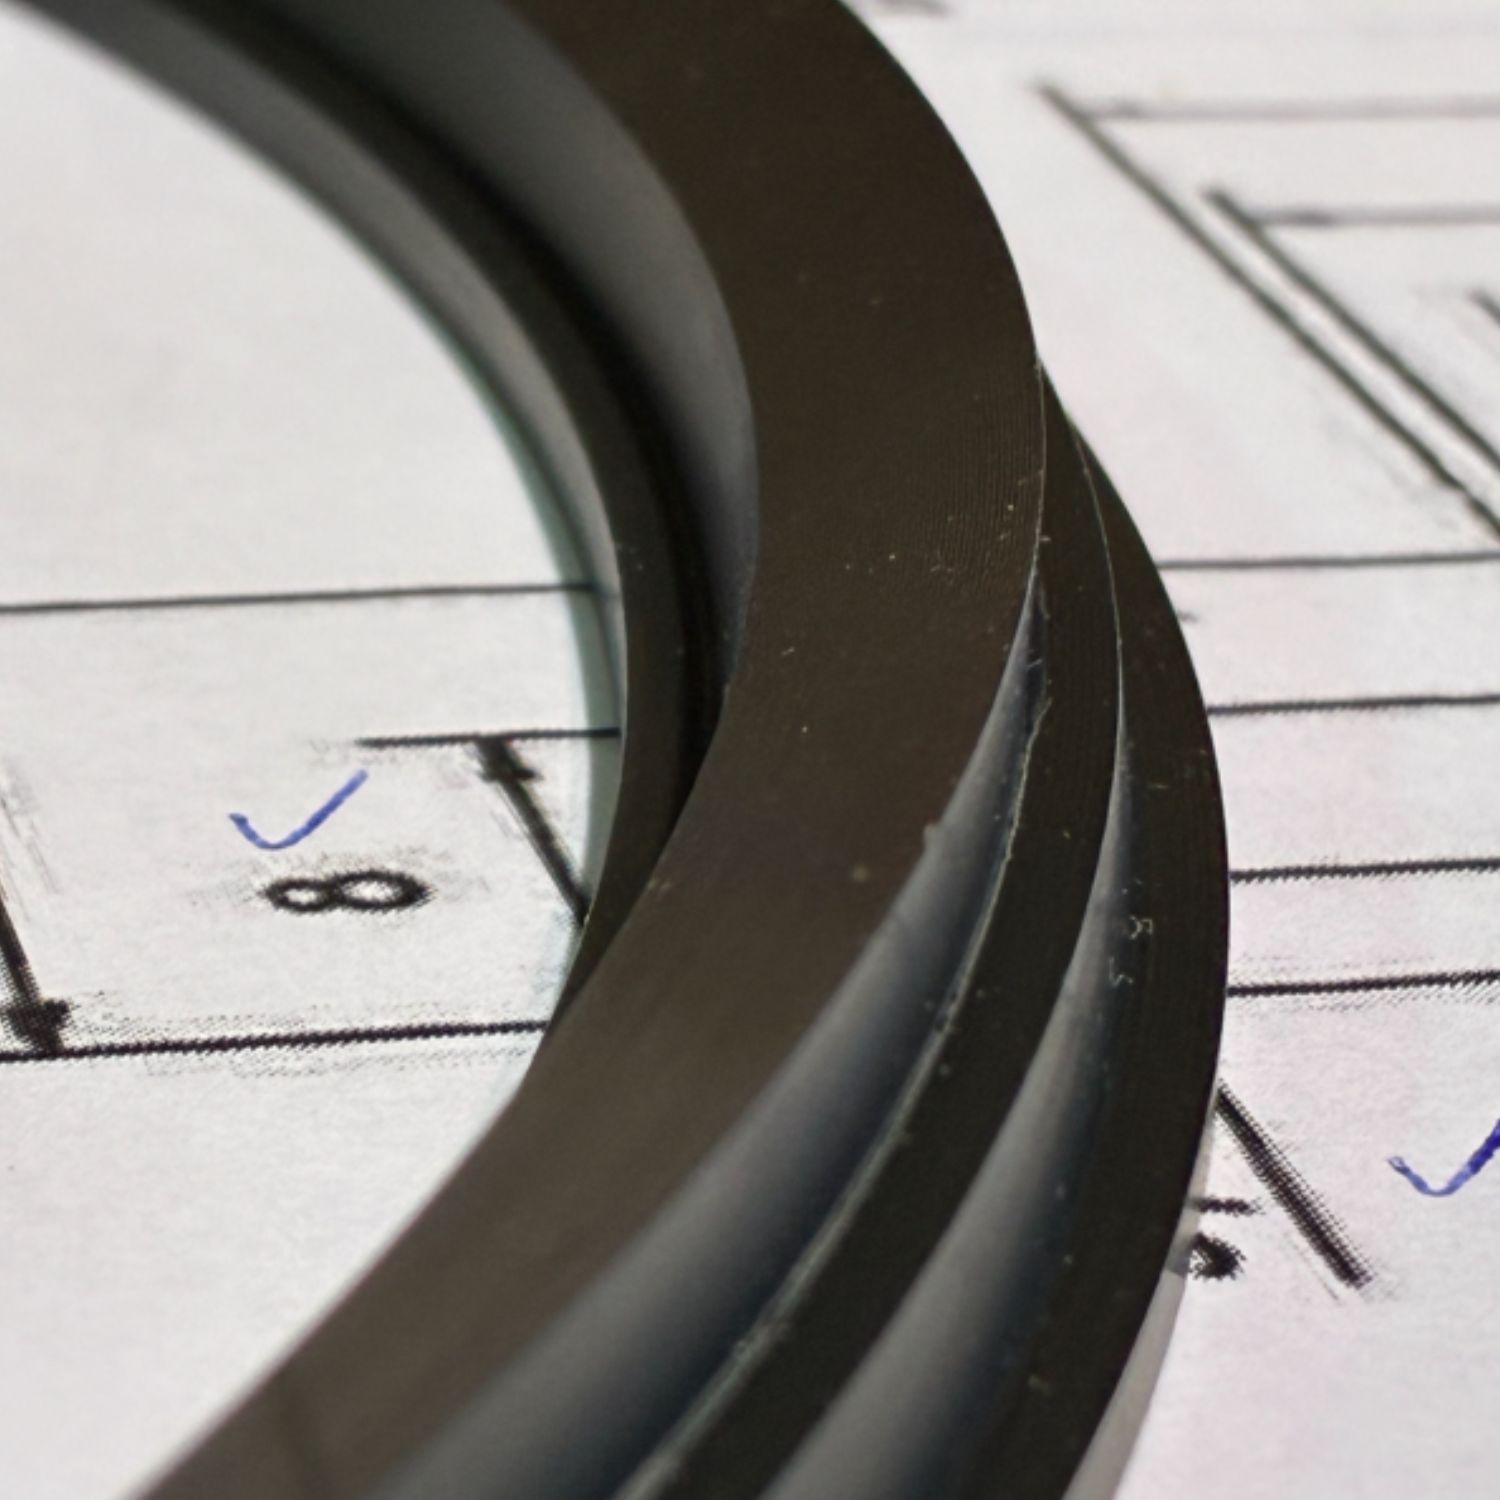
Collaborative design — example: double-lip urethane axial seal
Custom seal design is a collaborative process. The example below shows a double-lip urethane axial seal developed in partnership with a customer who needed simultaneous radial and axial sealing in a confined space that no standard seal could fill.

The design process typically follows: application analysis → sealing concept development → 2D cross-section drawing → FEA compression simulation (where needed) → prototype mold → prototype validation → production mold → PPAP / first article inspection → production release.
Materials
Molding compound selection
NBR (Nitrile)
EPDM
Silicone (VMQ)
FKM (Viton®)
Urethane (PU)
HNBR
Neoprene (CR)
Thermoplastics (PA, POM, PEEK)
Have a sealing problem that needs a custom solution?
Share the application details, the failure mode of your current seal, and any dimensional constraints — we'll develop a design proposal and quote from concept to production.
Start the Design Discussion